Hardness Testing Methods and Acceptance Criteria for Rubber Screen Plates
For mineral processing, aggregate and industrial screening operations, inconsistent rubber hardness across different batches of screening media often leads to completely unpredictable service life, with some panels wearing through in a fraction of the advertised time while others turn rigid and lose their anti-clogging flexibility far too early. Many operations that never verify hardness on delivered batches ended up wasting thousands of dollars on underperforming panels that failed long before their expected replacement date, with no clear way to trace the quality issue back to the material formulation. Standardized hardness testing methods and clear acceptance criteria for Rubber Screen Plates eliminate this hidden quality risk, making sure every batch you receive meets the exact performance specification your operation requires.
Shore A Hardness Spot Testing on Production Batch Samples
The first most widely used and practical testing method uses a standard Shore A durometer, pressed firmly vertically into the flat, non-abrasive main surface of randomly sampled Rubber Screen Plates from each new production batch, taking readings at 5 different evenly distributed points across the panel to get a representative average value. This test is fast, low-cost and easy to carry out both in the supplier’s factory and on your own site after delivery, so you can quickly confirm the rubber hardness falls in the expected range without needing complex lab equipment.
How the Reading Is Actually Taken
The everyday method for a Rubber Screen Plate is the Shore A durometer, done against ASTM D2240 or ISO 7619-1, and the result is only as honest as the setup. The panel or coupon needs to sit on a hard flat backing, the surface has to be clean and dry, the indenter has to land away from ribs, apertures, cut edges, and the steel insert hiding under the rubber. Thin panels are the classic trap: standards want roughly 6 mm of rubber under the indenter, so a 20 mm deck is fine, but a 3 mm skin over a steel frame will read soft because the indenter feels the metal through the compound—what labs call a base-support or backing effect. Good practice is to take five or more points across the working face, throw out edge readings, average the rest, and report the spread, because uniformity matters as much as the average. For critical specs, IRHD testing per ISO 48 gives better repeatability on thicker compounds, and Shore D enters the conversation only when the material drifts into very hard wear compounds. A Rubber Screen Plate that passes on one lucky poke but varies eight points across the face is not a good panel with bad luck—it is a poorly cured, poorly mixed, or poorly designed part wearing a good number.
Sampling the Real Part, Not Just the Coupon
Factory QC love a "standard slab" because it always tests nicer than the product. The slab was cured in a clean mold, at the right temperature, with no steel skeleton, no aperture ligaments, and no thick-to-thin transitions. A real Rubber Screen Plate is none of that: feed-end zone is thick, discharge zone is thin, apertures create local strain, steel inserts steal heat during vulcanization, and the corner that sits near the sprue often cures harder than the far corner. So acceptance testing has to include production panels, not just companion plaques. One practical routine is to measure the same grid of points on every sampled plate—say three points in the feed zone, three mid-deck, three discharge—and log them by serial number, so a later complaint can be matched to the exact panel that shipped. If the supplier refuses to test the actual Rubber Screen Plate and only offers "lab slab 62 Shore A," the buyer should hear that as "we do not want you looking at the real part." Companion slabs confirm the compound; production-panel mapping confirms the product.
Setting the Acceptance Band by Duty
A single universal tolerance for a Rubber Screen Plate is nonsense, because rubber screening duties pull in opposite directions. Sticky fine coal, washed sand, deslime decks, and dewatering faces want flexibility, often around 45–60 Shore A, so the aperture mouth flexes and ejects near-size slime instead of welding it shut. Primary scalping, ROM ore, granite, basalt, and recycled concrete want impact and cut resistance, so the compound drifts toward 65–80+ Shore A, sometimes with steel cord or insert reinforcement. The acceptance criterion should therefore be written as a duty-specific band: dewatering rubber 50 ± 5 Shore A, general aggregate screen 60 ± 5, heavy-impact scalper 72 ± 5, and so on. Industrial rubber parts commonly run ±5 Shore A, while tighter process control targets ±3; a Rubber Screen Plate supplier promising "exact number every time" is either rounding hard or not telling you about the rejects they buried. The smarter spec also sets a uniformity rule—max spread across one panel, say no more than 5 points—because a panel that averages 60 but ranges 54–66 will blind in one zone and chunk out in another.
Post-Aging Hardness Retention Verification
The second critical testing step takes test samples from the same batch and places them in a controlled thermal aging chamber for 72 hours at 70 degrees Celsius, then re-tests their Shore A hardness to measure how much the material hardens after simulating long-term exposure to normal operating heat. This test filters out low-quality rubber blends that will turn excessively brittle and lose elasticity quickly on the screening deck, ensuring the Rubber Screen Plates you use will retain enough flexibility to deliver reliable anti-clogging performance across their full service life.
Site-Specific Custom Acceptance Threshold Setting
The final most practical best practice is to set your own tailored hardness acceptance range based on your site’s unique operating conditions, rather than using a generic one-size-fits-all standard. Operations processing sharp, high-abrasion ore can set a slightly higher Shore A hardness threshold to get better wear resistance, while sites handling sticky, near-size fine material can specify a slightly lower hardness range to maximize the flexible anti-blinding performance of their Rubber Screen Plates.
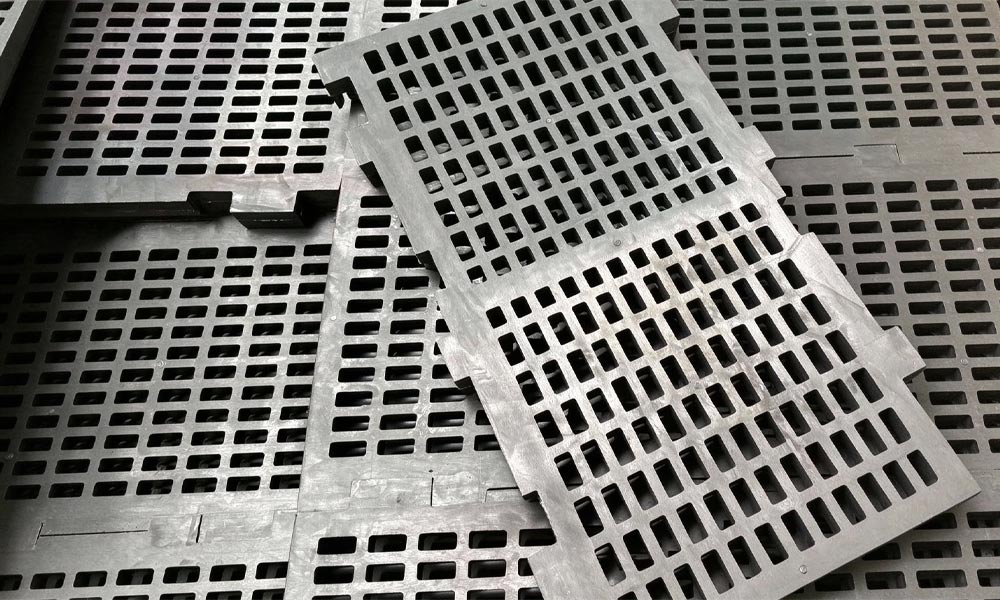
Following these clear hardness testing steps and setting appropriate acceptance criteria for your site will help you filter out low-quality inconsistent batches, drastically reduce premature panel failures, and make sure every unit you install delivers the expected service life. If you share details of your site’s typical processed material type and operating temperature range, our technical team can help you work out the exact optimal hardness acceptance range for your specific working conditions.