Wear-Resistant Formulation Design and Replacement Cycle of Woven Metal Screens for Copper Ore Processing
In copper ore processing, screening operations face some of the most abrasive conditions in mineral beneficiation. The sharp, hard particles in crushed copper ore rapidly wear down standard screening media, leading to frequent replacements, high costs, and production interruptions. Selecting the right woven metal screens with a wear-resistant formulation and establishing a data-driven replacement cycle are therefore critical strategies for maximizing screen life, controlling operational expenses, and maintaining consistent throughput in your copper concentrator.
Selecting the Right Alloy for Abrasive Duty
The foundation of wear resistance in woven metal screens lies in the wire alloy. For copper ore applications, high-carbon steel is a common and cost-effective choice, offering good abrasion resistance through its hardened structure. For more severe duty or where corrosion from process water is also a concern, martensitic stainless steels like 410 or 420 provide a superior balance of hardness and corrosion resistance. In highly corrosive and abrasive slurry environments, premium alloys like 316 stainless steel may be justified despite higher initial cost, due to significantly extended service life. The key is matching the alloy’s hardness and corrosion properties to the specific abrasiveness and pH of your ore.
Alloy Formulation Starts With the Ore Chemistry
Most copper concentrators begin the screen-media conversation at the wrong end, asking "304 or 316?" when they should be asking "what is in my slurry and how hard is the rock hitting the deck." High-carbon spring steel such as 65Mn gives excellent abrasion and fatigue behavior in dry or lightly corrosive copper circuits, and it remains the workhorse for coarse scalping because the wire can be quenched and tempered into a hard, resilient crown that shrugs off repeated impact. Manganese steel variants such as Mn14 or Mn18Cr2 earn their place where lump size is large and impact dominates, because the surface work-hardens under pounding while the core stays tough. The moment the circuit turns wet—thickener overflow recycle, flotation tailings return, acidic process water, sulfate- and chloride-laden slurry—plain carbon steel starts corroding first and abrading faster because corrosion roughens the wire and gives abrasive particles somewhere to bite. That is where 316L becomes the practical compromise: molybdenum improves pitting resistance, and the screen keeps its aperture longer in copper slurries that would eat 304.
Weave Geometry Is Part of the Wear Formula
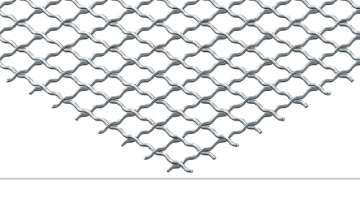
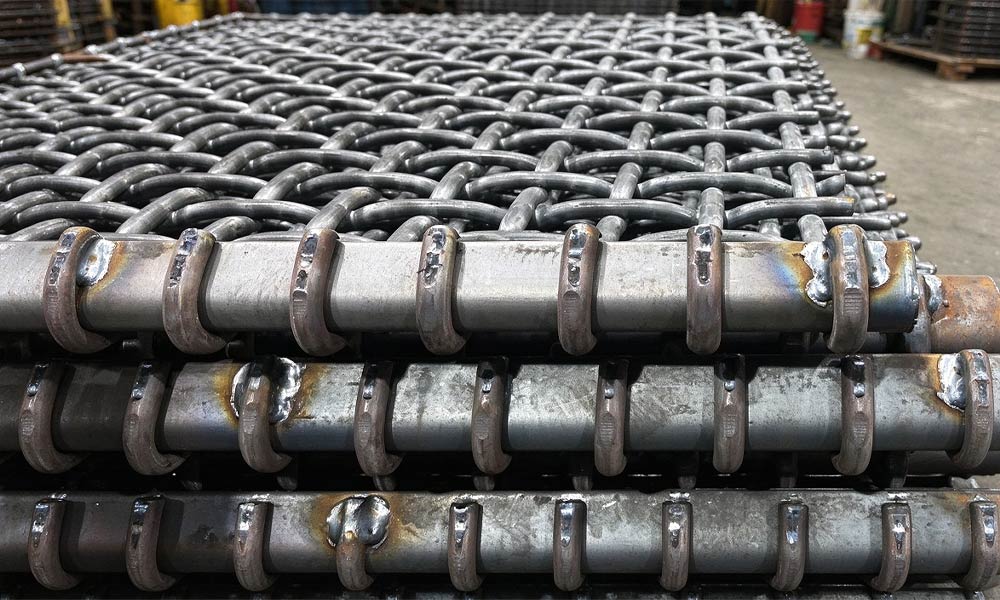
Alloy gets the attention, but the weave is what decides whether the wear is spread evenly or concentrated at a few doomed intersections. Lock-crimp and double-crimp constructions lock the wires so they cannot slip sideways under vibration, which keeps aperture deviation small even after thousands of hours of pounding—critical in copper milling, because a Woven Screens deck that opens up by 5% starts sending coarse rocks into the ball mill and turns power draw into noise. Flat-top weaves reduce crevices where corrosive slurry pools, so they suit finer copper classification decks where pitting at the wire crossing is the real killer. Wire diameter is treated like a wear budget: a plant that specs the minimum wire to maximize open area often buys a few extra tonnes per hour and pays for it with a halved service life, while adding 0.3–0.5 mm of wire diameter gives a wear allowance that costs little in throughput but can add weeks of deck life. Hook edge and tensioning are the silent contributors to wear too—an under-tensioned Woven Screens panel drums, the wires flex in the wrong plane, fatigue cracks start at the selvage, and the panel fails long before abrasive wear would have ended it.
Building the Replacement Cycle From Wear Data
The old habit—run the screen until it breaks, then swear at the storeroom—is the most expensive option on a copper circuit, because unplanned changeouts cost production time, let off-spec material reach downstream, and often damage the support frame when a torn panel flaps under full stroke. A wear-based replacement cycle starts by logging, not guessing: aperture at commissioning, wire-crown thickness at the feed end, tonnes screened per shift, moisture band, chloride/sulfate levels, deck amperage, blinding area, and oversize-in-undersize percentage. After two or three panel histories the plant can predict remaining life from cumulative tonnes and feed hardness instead of from a calendar. A Woven Screens panel on a Chilean or Peruvian copper scalper might be pulled at a planned shutdown when crown loss hits a set threshold even if it still "looks usable," because the money saved by squeezing another week is dwarfed by the cost of milling oversize or stopping the crusher at peak throughput. In abrasive copper applications screen media can be replaced every 6–12 weeks, while finer classification decks with better alloy and heavier wire may run several months; the number is site-specific, not catalogue-specific.The replacement rule that works in practice is simple: change before efficiency drops below the product spec, change during a planned window, and never let the same panel reach the point where wires snap at the hook.
Optimizing Wire and Weave Design for Longevity
Beyond material, the physical design of the woven metal screens plays a major role. Increasing the wire diameter directly adds more wear material, prolonging life but reducing open area. A strategic approach is to specify a heavier wire gauge on the top side of the screen in a double crimp or lock crimp weave. This weave style locks the wires firmly at each intersection, preventing them from moving independently under load, which reduces notch wear and wire fatigue. The result is a screen that maintains its structural integrity and opening size longer under the punishing impact of copper ore.
Determining a Cost-Effective Replacement Cycle
Establishing the optimal replacement cycle for woven metal screens in copper processing is not about running them until failure. It involves monitoring performance indicators such as a noticeable decrease in screening efficiency, an increase in “oversize” reporting to the undersize stream, or visible wear patterns that threaten panel integrity. Weigh the cost of a new screen against the cost of lost production and degraded product quality from a worn screen. Implementing a planned, preventative replacement schedule based on historical wear data is far more economical than reacting to an unexpected screen breakdown during a critical production run.
For copper processors, viewing woven metal screens as a consumable with a calculated lifespan is essential. By specifying the optimal wear-resistant alloy and weave design for your specific ore characteristics, and then replacing screens based on performance data rather than catastrophic failure, you transform screen cost from a variable expense into a predictable, optimized component of your operating budget, ensuring smoother and more profitable plant operation.