The Complete Production Process for Woven Metal Screen: From Raw Wire to Finished Screen
Most people grab a roll of woven metal mesh and never think twice about what went into it. But behind every panel sitting on a vibrating screen is a production process that's more precise than you'd guess. From raw wire drawing to the final tensioned sheet, dozens of steps decide whether your finished screen mesh holds up under pressure or falls apart after a month. Here's the full picture, no fluff.
Wire Drawing: It Starts Thinner Than You Think
Everything begins with wire rods, stainless steel, carbon steel, or specialty alloys pulled through a series of dies. Each pass shrinks the diameter a little more until you hit the exact gauge you need. For most woven metal mesh, that's anywhere from 0.5mm to 6mm depending on the application. The drawing process also hardens the metal slightly, which matters later when the wire gets bent and woven under tension.
Wire Rod Selection and Drawing: The Tolerance Is Set Before Weaving Starts
Everything begins with the rod, not the loom. Stainless 304, 316L, 310, duplex, high-carbon steel, 65Mn, galvanised wire or exotic alloys each bring a different starting temperament, and the drawing process has to respect that. The rod is pulled through progressively smaller dies, sometimes with inline laser gauging, until the wire hits the exact diameter the mesh spec demands — anything from fine micron-grade filament to 6 mm-plus screening wire. Cold drawing hardens the surface and tightens tensile strength, which is great for wear life but dangerous if the wire becomes brittle, so many mills anneal between passes or at the end to restore ductility. A Woven Wire Mesh made from uneven-diameter wire will never screen true: the reed cannot space the warp evenly, the weft cannot seat consistently, and the aperture tolerance drifts before the panel leaves the factory. Good mills treat wire diameter, ovality, surface finish and draw lubricant residue as quality variables, not afterthoughts.
Annealing, Cleaning and Straightening: Getting the Wire Loom-Ready
After drawing, the wire is often work-hardened, oily and not perfectly straight — three problems that wreck weaving. Annealing in a controlled-atmosphere furnace softens the wire without oxidising the surface, especially important for austenitic stainless where chrome must stay available to form the passive film later. Then comes cleaning: ultrasonic baths, alkaline degreasing or solvent stages strip drawing lubricants that would otherwise burn into the mesh and contaminate a food- or pharma-grade screen. Straightening rolls remove the natural helix from coiled wire so the warp feeds true. A Woven Wire Mesh that blinds prematurely or frays at the edge often traces back to this unglamorous stage — the loom was asked to weave wire that was never actually ready to be woven.
Crimping: Where Heavy-Duty Screens Get Their Backbone
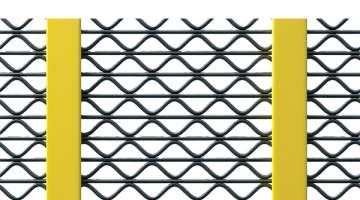
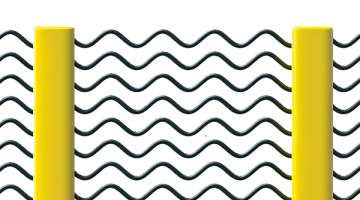
For coarse screening mesh, crimping is the step people underestimate. Pre-crimping puts a controlled wave into warp and weft before weaving, so the wires lock at the intersection instead of creeping under vibration. Plain crimp, double crimp, lock crimp, intercrimp and flat-top each exist for a reason: lock crimp stabilises big coarse apertures on vibrating decks, flat-top keeps the wearing surface smooth for material flow, intercrimp supports fine wire with large openings. The crimp pitch and depth have to match between warp and weft, or the panel will look fine on the table and then “grow” apertures once the deck starts shaking. A Woven Wire Mesh for mining, quarry or aggregate duty without proper crimping is basically a sieve waiting to lose its cut point — the wires migrate, the holes enlarge, and the metallurgist blames the ore when the media was never stable.
Weaving: Where Pattern Meets Purpose
This is where it gets interesting. Industrial looms interlace warp and weft wires in specific patterns such as plain, twill, Dutch, or reverse Dutch, each offering different open area and strength characteristics. A plain weave is tight and durable; a twill weave flexes more and resists fatigue. The loom speed, wire tension, and crimp settings all get dialed in based on what the finished woven wire screen needs to do. One wrong setting and you get an uneven panel that nobody wants.
Finishing Touches That Make or Break Quality
After weaving, the woven screen gets heat-treated to relieve stress, cleaned to remove oils, then tensioned on a leveler so it lays flat without warping. Edge trimming and final inspection come last—checking for broken wires, inconsistent apertures, or surface defects. Quality control here separates industrial-grade mesh from the junk that ends up in discount bins.
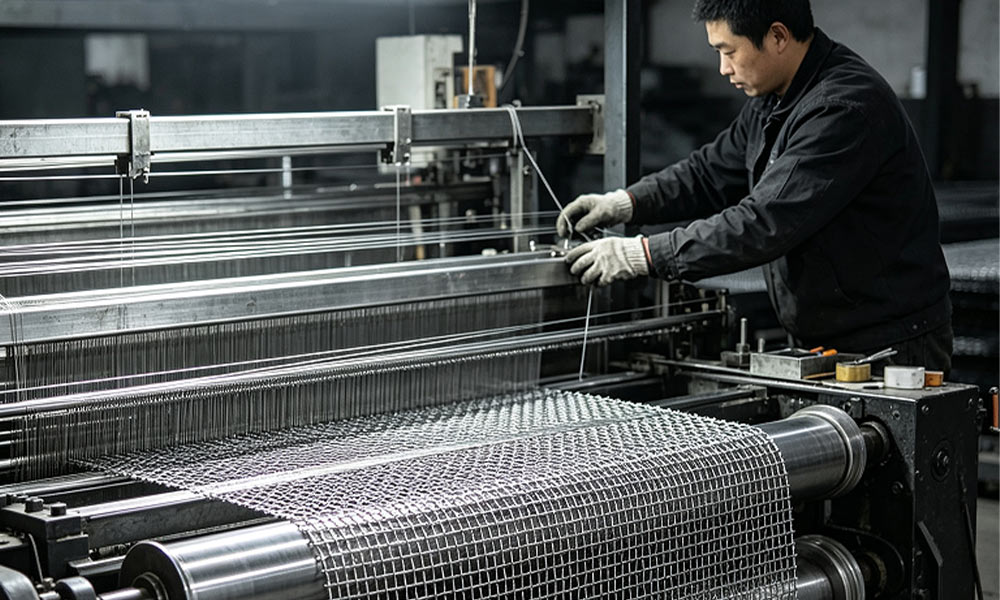
Understanding the complete production process for woven metal mesh helps you buy smarter, not cheaper. If you need a custom spec, unusual alloy, non-standard aperture or specific crimp for example, the right manufacturer will walk you through every stage. Tell us what you need and we'll connect you with someone who actually knows their loom from their loader. Contact our engineering team for custom woven metal mesh solutions.