Third-Party Quality Testing of Self-Cleaning Screens: Target Values for Screening Efficiency and Wear Resistance
For mineral processing operations that rely on self‑cleaning screens to maintain stable high‑throughput classification without frequent manual deck cleaning, independent third‑party quality testing is the most reliable way to confirm that newly delivered panels meet advertised performance claims, instead of discovering hidden quality flaws only after installation causes unexpected production losses. Many operations skip this formal verification step and only do basic visual checks on delivery, only to find their new screens cannot hit the required screening efficiency or wear out far faster than promised, wasting significant spare parts budget and production uptime. A standardized, independent Self‑Cleaning Screen Quality Testing process with clear, industry‑aligned target values for core performance metrics eliminates these hidden risks completely, giving operations full confidence in every new screen panel they put into service.
Standardized Screening Efficiency Test Conditions
The first core section of a rigorous Self‑Cleaning Screen Quality Testing workflow runs under real‑world simulated operating parameters, using the exact material particle size distribution, feed volume, vibration frequency and deck angle that the screen will encounter on site, to avoid the inflated efficiency numbers that come from unrealistic lab‑only test conditions. This test measures the percentage of target‑sized particles that correctly pass through the screen apertures, while tracking how often near‑size particles get wedged in the openings and reduce effective open area over extended continuous operation.
Screening Efficiency Targets That Mean Something
Screening efficiency is not a single magic percentage; it is a material-balance question. The laboratory version usually measures recovery of undersize to the underflow and recovery of oversize to the overflow, then multiplies them into an overall efficiency. For a self-cleaning deck on wet, sticky, or near-size-heavy feed, a reasonable third-party acceptance band is around 85–95% overall efficiency on a representative feed, while a difficult near-size-dominated feed may be planned for 75–85% and still beat a blinded woven deck that has slipped into the low-60s after an hour of moisture. The smarter metric for self-cleaning media is not the opening number but the sustained number: a good panel should hold 85%+ of its effective open area across an 8-hour shift, whereas a poor one can lose more than half its open area inside the first hour once slime starts bridging the slots. Misplaced-material content matters just as much—fines in the oversize stream and coarse in the undersize stream should be quantified, because a self-cleaning screen that keeps flowing but ships oversize into flotation is simply trading blinding for grade penalty. A credible Self-Cleaning Screen Quality Testing report therefore includes feed size distribution, product size distribution, near-size ratio, moisture, bed depth, stroke, and a partition curve, not just a happy “passed” stamp.
Wear Resistance: Elastomer Numbers, Not Marketing Words
Behind every self-cleaning panel is a polyurethane or rubber compound, and compound quality is where suppliers quietly diverge. Third-party wear testing should start with Shore A hardness to ASTM D2240, because most mining PU screen media lives in the 80–92 A band: too soft and the ligament rolls under load, too hard and the panel loses the flex that makes it self-cleaning. Abrasion resistance belongs in the file as ISO 4649 volume loss in mm³, with the abrasive grade, specimen prep, and drum condition stated—because comparing one supplier’s “good” number to another supplier’s unspecified method is how buyers get fooled. Tensile strength, elongation at break, tear strength per ASTM D412 / ASTM D624, rebound resilience, compression set, hydrolysis resistance for wet duty, and chemical resistance for reagent-laden slurries should all be there for a real spec. A practical PU screen panel might show tensile in the 25–40 MPa range, tear in the 80–120 kN/m range, and ISO 4649 loss in the 30–45 mm³ band, but the target is always relative to duty: a chrome-ore deck cares more about cut/abrasion, a wet coal deck cares more about hydrolysis and anti-pegging, and a quartz line cares more about low contamination and tight aperture stability. Self-Cleaning Screen Quality Testing that omits tear and rebound is like buying a tire by tread color—pleasant, irrelevant, and expensive later.
Field Trial Is the Part Suppliers Fear
Lab sheets prove the compound; they do not prove your plant. The third-party step that actually protects the budget is a tagged field trial with reason-for-removal logged every time. The panel goes on the real deck, in the real ore, with the real spray water and the real 2 a.m. feed surge, and someone records open-area loss at 2, 4, 8, and 24 hours, aperture enlargement in millimeters, peg count per square meter, underside slurry buildup, side-seal compression loss, and tonnes screened per millimeter of crown wear. A Self-Cleaning Screen Quality Testing protocol worth signing says something blunt: remove the panel if aperture exceeds 15–20% of nominal, if open area drops below the agreed floor, if tears reach the support bar, or if product size distribution drifts outside the plant’s metallurgical tolerance—not “when it falls through.” Wear rate should be reported as millimeters lost per 1,000 tonnes or as changeout interval versus the incumbent media, because Shore A alone never told a plant manager when to order the next container. The best third-party reports end with a cost-per-screened-tonne comparison, not a medal, because the screen’s job is not to pass a test—it is to keep the circuit making saleable product while the maintenance crew sleeps.
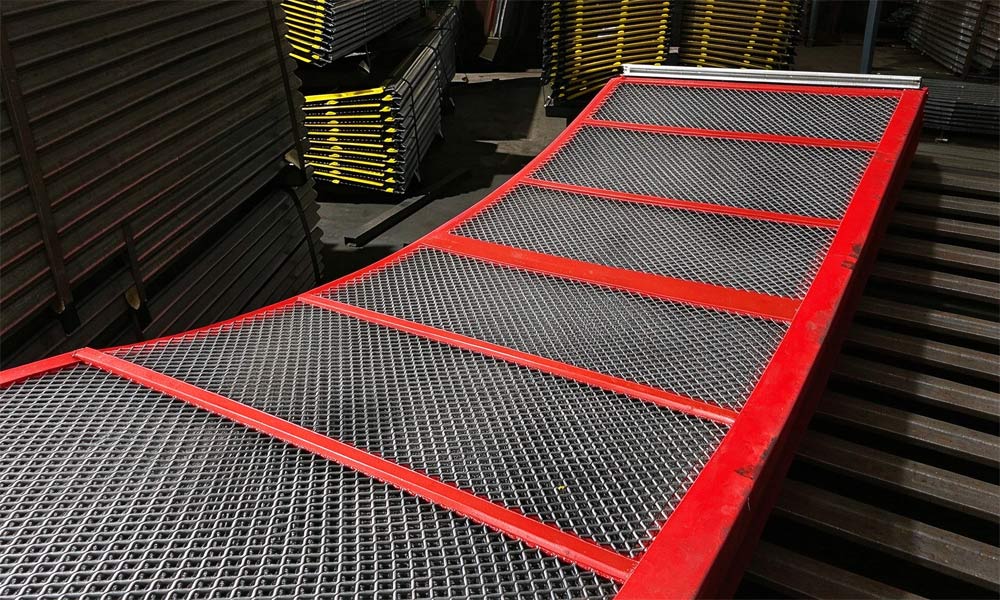
Industry‑Aligned Screening Efficiency Target Values
For most industrial mineral processing applications, a qualified self‑cleaning screen should deliver a minimum 95% stable screening efficiency after 2 hours of continuous full‑load operation, with no more than 3% drop in efficiency from the initial start‑up value, even when processing high volumes of near‑size particles that easily clog standard rigid screen panels. This target value is calibrated to ensure the screen maintains consistent classification performance across long production cycles, without requiring frequent stops for manual deck cleaning to dislodge stuck particles.
Verified Wear Resistance Benchmark Targets
The wear resistance segment of proper Self‑Cleaning Screen Quality Testing runs continuous high‑abrasion material feed for a standardized 72‑hour test period, measuring the total surface material loss and checking for any signs of surface fatigue cracking or deformation on the self‑cleaning flexible elements. A performance‑qualified panel should show less than 0.2mm of average surface wear depth after this test, with zero visible cracking or structural deformation, confirming it can deliver the full advertised service life even under 24/7 continuous high‑abrasion operating conditions.
A properly executed independent Self‑Cleaning Screen Quality Testing process with clear, practical target values for screening efficiency and wear resistance eliminates almost all the quality uncertainty that comes with sourcing new self‑cleaning screen panels, drastically reducing the risk of unexpected performance drops and premature failure on your production line.