Identification and Acceptance of Common Manufacturing Defects in Polyurethane Screen Panels
For plant operators, identifying manufacturing defects in new polyurethane screen panels is crucial to avoid premature failures. A systematic acceptance check ensures you install panels fit for purpose, not just new ones.
Visual Inspection: Surface and Aperture Integrity
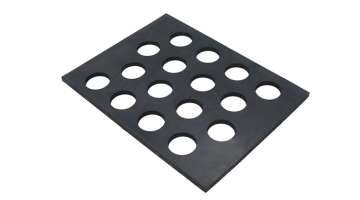
Product inspection requires both visual and tactile checks performed under adequate lighting. Inspect for the presence of air bubbles or pinholes. While the occasional appearance of a few small bubbles is normal, an excessive number of bubbles—or bubbles located on the apertures—can lead to screen breakage and directly compromise screening performance; such units must be rejected. When examining the surface of the polyurethane screen panel, verify that each aperture is uniform in shape and features a clean, consistent taper. Apertures with irregular shapes or rough edges reduce screening efficiency and cause issues such as clogging and uneven wear; these are classified as defective products.
Difference Between a Blemish and a Blinding Risk
The first inspection of a Polyurethane Screen should happen in good light with a caliper, a Shore-A durometer, and a skeptical eye, because the working face is where small defects stop being cosmetic. A few tiny pinholes on a thick non-working area may be acceptable, but bubbles sitting on or near the aperture walls act like little ledges for fines and brine, so a sticky iron-ore or potash feed will happily nucleate a clog right where the bubble left a thin spot. Surface softness or tackiness is a louder alarm: polyurethane that has not fully cross-linked feels sticky or unusually spongy, wears fast, and loses tear strength under vibration, which means the panel may look new on Monday and look chewed by Thursday.Aperture uniformity is the other non-negotiable—each slot or square should carry the same taper, the same width, and the same crown radius, because a Polyurethane Screen does not blind uniformly, it blinds where one row of holes was molded 0.15 mm too tight and the rest of the deck keeps flowing. Edge flash, burrs, broken rib tips, and color streaks from poor mixing are not glamour problems; they are clues that the mold temperature, degassing, or raw-material batch was not under control, and the same instability that made the streak can also have hidden the void you cannot see.
Why the Fixing Zone Fails Before the Wear Face
Most premature Polyurethane Screen failures are not caused by the screening surface at all—they start at the steel skeleton, the hook strip, the bolt boss, or the cassette latch, because that is where a soft elastomer has to grip a hard metal part that never wanted to be gripped. A weak chemical bond between polyurethane and the embedded steel lets the polymer delaminate under millions of vibration cycles; once the polyurethane starts sliding on the insert, the hook flexes on its own, fatigue cracks walk in from the bend, and the panel comes loose while the wear face still looks almost new.Acceptance here means more than “does the bolt hole line up”: press the boss, check for movement between PU and steel, look for rust bleeding from a poorly sealed insert, and reject panels where the insert sits proud or the hook reinforcement looks thin. On tensioned screens, the hook is the most abused part of the whole Polyurethane Screen, so a hook with a cold-shut weld, a sharp bend radius, cheap carbon steel in a corrosive circuit, or inadequate surface preparation before molding should be treated as a structural defect, not a finishing detail. A plant that accepts “nice looking face, dodgy hook” is basically buying a screen whose strongest argument is photography.
Dimensional and Structural Soundness
Check for warping by placing the panel on a flat surface. Any significant rocking or bow prevents even tensioning, leading to high stress and early failure—a clear reject. Use calipers to verify thickness consistency. Variations beyond the stated tolerance indicate poor molding and cause uneven wear. For reinforced Polyurethane panels, ensure steel or fabric is fully encapsulated and centered. Exposed reinforcement or delamination is a critical structural failure and is never acceptable.
Material Consistency and Cure Quality
Feel for areas that are softer or tacky compared to the rest of the panel. These “soft spots” signal incomplete curing, resulting in low hardness and poor wear resistance, and are not acceptable. Also check for embedded foreign particles. While a deep, minor speck might be tolerated, significant contamination on working surfaces or edges creates a weakness and is usually grounds for rejection.
The goal of Inspecting the quality of the polyurethane screen panels is to prevent functional failures, not seek perfection. Create a simple checklist based on these defects. For critical applications, enforce stricter tolerances. Always refer to the supplier's quality specs. For borderline cases, photograph the defect and consult the supplier. Focus on rejecting panels with flaws that will directly impact safety, performance, or service life in your specific operation.